


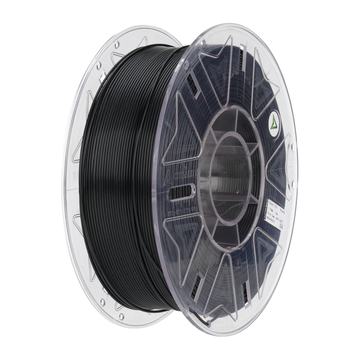
You want a model to come out right the first time, without endless tweaking. It makes sense. With Polymaker, you choose filament that prints predictably while leaving room for growth, from rapid prototypes to polished final models. In this article, AC PRODUCTS shows you how to achieve consistent quality with the right material choice, sensible settings, and a smart workflow, even when the deadline is approaching.
Why consistency is more important than a lucky top print
A single perfect print is nice, but repeatability is what counts for your planning. Polymaker is known for even extrusion and precise diameter control. You notice this in clean walls, well-fitting snaps, and less post-processing. Those who manage projects want predictable parameters per part type, not guesswork. By working with fixed profiles per material and part, you achieve speed without surprises. This keeps the first layer reliable and ensures details hold up even at higher speeds.
Which line suits which project
You don’t have to be a materials expert to make better choices. Think in terms of use: display model, functional prototype, assembly aid, or final part. Polymaker provides a suitable base for every purpose, from easy-to-print PLA variants to engineering plastics with extra heat resistance or impact strength. It helps to separate form and function: manage the appearance with layer height, wall thickness, and cooling, and the strength with material choice, infill, and orientation. If you choose a clear goal for each part, the material selection becomes logical automatically.
Quick choices based on application
- Display models and fitting tests: choose an easy-to-print PLA or PETG for speed and clean surfaces that require little post-processing.
- Functional prototypes with clips or hinges: go for a tough variant or an impact-resistant plastic with higher heat resistance.
- Flexible inserts and dampers: use TPU with a shore hardness that suits the load, print slowly, and ensure proper filament drying.
- Mechanical parts and fixtures: choose an engineering plastic or a fiber-reinforced variant, and pay attention to nozzle diameter and abrasive wear.
- Outdoor or workshop floor: look for materials that can better withstand UV or chemical stress and adjust cooling and chamber temperature accordingly.
Quickly towards a predictable workflow
The gain lies in preparation. Create a base profile for each material with three layer heights that you actually use. Add three things to each profile: a proven brim or skirt strategy, a safe retraction value, and a first-layer routine that you don't have to think about every time. Polymaker gives you the stability; you add the discipline. Choose one recipe per part and stick to it for predictable results. If you want to scale up later, you only need to choose which nozzle and which batch you use, not how to print.
Finishing without the hassle
Finishing is more than sanding. With the right print settings, you save half the post-processing time. Work with clean wall multiples so seams close nicely and place the z-seam intentionally on a corner or inward. Some PVB-based lines from Polymaker can be smoothed with an alcohol mist, which gives display models an almost molded appearance. For technical parts, a light flame or hot air treatment is sometimes enough to soften edges. If you are printing multiple colors, place transition points out of sight and keep purge towers compact.
Drying, storage, and stability
Many print problems are not slicer errors, but moisture in the filament. Store spools in a dry place, preferably in a box with desiccant and a hygrometer. If necessary, heat for a few hours at a low temperature according to the material guidelines. Polymaker supplies many spools vacuum-packed and neatly sealed, yet it pays to treat opened spools consciously. Store your filament dry and do not continue printing if the spool is noticeably damp. It prevents stringing, matte spots, and poor layer adhesion—precisely the things that disrupt your turnaround time.
Sustainability and packaging
More and more users want results and less waste. Various lines come on cardboard spools and in sober, easily recyclable packaging. That is not only considerate, but also practical on the work floor. With Polymaker, you build a material stock step-by-step that is easy to manage, with clear labels and consistent batch information. Combine that with a simple FIFO system and you keep a grip on costs, quality, and warehouse space.
Common mistakes you can easily avoid
The biggest temptation with modern printers is to go too fast. Professional quality comes from controlled printing with the right cooling per geometry. Do not let bridges pull too quickly, give small details enough time, and keep the nozzle temperature stable. Another pitfall is approaching every print differently. With Polymaker, you don't need to vary settings to achieve quality. Use repeatable profiles and only adjust something when absolutely necessary. Finally: choose your nozzle consciously. Wear-resistant for fiber-filled materials, standard for PLA and PETG. It prevents inaccurate extrusion and saves you from searching for inexplicable dimensional differences months later.
AC PRODUCTS helps you from unboxing to the first batch
You want to deliver today, not test for weeks. AC PRODUCTS helps you in one session to create clean base profiles that fit your printer and parts. We look at layer height per function, wall thickness versus strength, cooling per bridge type, and build plate adhesion that works in your workspace. With Polymaker, we then fine-tune: just enough temperature, just enough flow, no exotic tweaks. With the right profiles, a first batch is achievable in the same weekend.
Ensuring quality within a team
If you don't print alone but work with colleagues, documentation is crucial. Create a simple card per part: material, nozzle, layer height, temperature, cooling, specific notes. Set up a bin with approved test pieces so everyone knows how it should feel and look. Use fixed filenames with version numbers and print settings. With Polymaker, you keep variables low and productivity high, even when multiple projects are running in parallel.
From challenge to routine
Every organization has parts that have remained difficult. Fine snap-fits, thin walls, large flat surfaces. Treat those as mini-projects. Test three settings, note everything down, choose the winner, and lock in the recipe. Through that approach, you shorten the learning curve dramatically. You will notice that you correct less in CAD and that supports come off better. In combination with Polymaker, precision becomes a habit. That is exactly what you need when customers ask more often and faster for visually convincing parts that are mechanically sound.
Conclusion: Professional results start with the right foundation
Those who want to print professionally don't have to make it complicated. Choose a reliable material base, create simple yet clean profiles, and execute them consistently. Polymaker gives you the stability to do that, and AC PRODUCTS ensures that you quickly turn that stability into results. This way, 3D printing becomes not an experiment per part, but a predictable production step that fits your planning and your customers.


Leave a comment